







Summary
A food preparation workflow audit converts an existing manual process into measurable information before equipment is selected. It records what enters each preparation stage, what acceptable output leaves it, how long the work takes, how many people participate, where material waits, how much yield is lost, what sanitation and changeover work is required, and how results vary across products, shifts and raw-material conditions.
The audit should cover complete production cycles rather than a single demonstration batch. Observations must be separated into measured data, calculated data, operator estimates and unresolved assumptions. This distinction matters because an apparently precise equipment brief may still be unreliable when it is based on nominal recipes, average daily output or unverified labor estimates.
The final deliverable is not simply a list of machines. It is a scoped project brief defining raw materials, finished specifications, required throughput, yield expectations, hygiene classification, available utilities, space constraints, operating hours, changeover requirements and acceptable automation levels. That brief helps a central kitchen, fresh-cut processor, food manufacturer or RTC/RTE facility compare manual, semi-automatic and integrated-line options on the same basis. It also reveals situations in which better scheduling, standardized work or a limited equipment upgrade may be more appropriate than full automation.
Why Equipment Selection Should Begin on the Production Floor
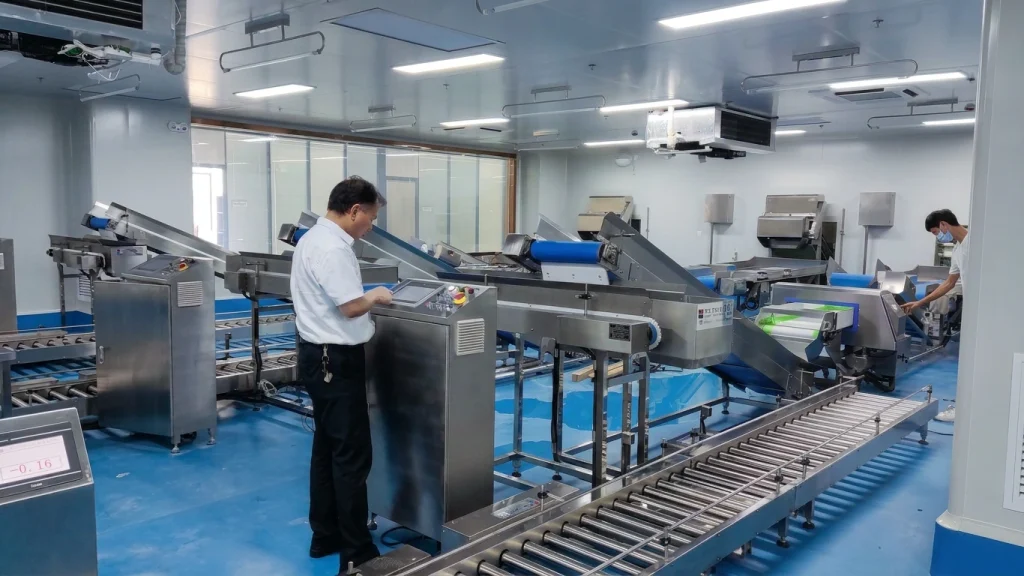
A production manager may describe the problem as “we need a faster vegetable washing machine.” During an actual shift, however, the washer may spend part of the day waiting for manually trimmed product, part operating below its useful load and part blocked because the dewatering or packing station cannot accept more output. Increasing washer capacity would create a larger queue rather than higher finished-product output.
The same problem appears in cutting, peeling, sorting and mixing. A machine may perform its own operation faster than workers, yet the full process can remain constrained by loading, inspection, batch release, container movement, sanitation or downstream cooking. Buying from a catalog capacity alone treats one operation as though it were independent of the surrounding workflow.
A food preparation workflow audit addresses a narrower and more practical question: what information must be known before a defensible equipment requirement can be written? It does not repeat a general automation-priority framework, calculate only the hidden cost of manual labor or map the entire receiving-to-distribution system. Its purpose is to establish an evidence-based baseline and translate that baseline into project inputs.
The audit should therefore be completed before a supplier is asked for a final configuration. Suppliers can help test products and interpret process requirements, but they cannot reconstruct missing plant data from a daily production total and several product photographs.
What a Food Preparation Workflow Audit Must Produce
The finished audit should allow the project team to answer five questions without relying on informal impressions:
- What products, quantities and specifications must the preparation area deliver?
- What does each current process stage consume in labor, time, space, water and usable raw material?
- Where do variation, delay, rework, damage and yield loss enter the workflow?
- Which hygiene, occupational-safety and product-separation requirements constrain the solution?
- What equipment functions, capacities and operating conditions are actually required?
The audit output should contain a current-state process map, observation records, a data-quality register, calculated performance metrics, a loss and delay summary, a product-family matrix and a preliminary equipment brief. Photographs, annotated layouts and short operating videos can support the records, provided that site rules permit them and the images are connected to a specific observation rather than used as a substitute for measurements.
Set the Audit Boundary Before Collecting Data
An audit can become unmanageable if the team attempts to document every movement in the facility at once. Define the boundary around the preparation operations that may be affected by the proposed project. For vegetables, that boundary might begin when released raw material enters the preparation room and end when washed, cut and dewatered product is transferred to cooking or packaging. It may include sorting, trimming, peeling, cutting, washing, inspection, dewatering and internal conveying.
Include upstream and downstream interfaces even when they are outside the equipment scope. The preparation team needs to know how raw material is presented, how quickly it arrives and what downstream operation consumes the prepared output. A new cutting system cannot operate continuously if ingredients arrive in mixed containers without batch identification. A washer cannot sustain its nominal flow if the next operation accepts product only in small, intermittent batches.
Select representative production days
One quiet shift rarely represents the real operating requirement. Observe enough cycles to capture a normal day, a high-demand period and at least one meaningful product or supplier variation. Seasonal produce may differ in size, soil load, maturity, firmness and defect rate. Those differences can change inspection time, trimming loss, peeling performance, water demand and cutting quality.
Where practical, audit at least three production periods and record why they were selected. If a peak season cannot be observed, mark peak data as historical or estimated instead of presenting it as measured fact. This prevents forecast assumptions from being mixed with current-state observations.
Form a small cross-functional audit team
Production understands sequence and scheduling. Operators know where manual work becomes difficult. Quality personnel understand specifications, release rules and hygiene controls. Engineering or maintenance can identify utilities, access, drainage and service requirements. Procurement or finance can supply labor and material costs.
No single department sees the complete problem. A production-only audit may overlook sanitation and maintenance. An engineering-only audit can underestimate product judgment and rework. A purchasing-led assessment may reduce the discussion to price and rated capacity before the operational requirement is stable.
Map the Current Process at Task Level
Begin with the physical path followed by one representative batch. Do not map only department names such as “vegetable preparation” or “washing.” Record the actual task sequence:
Raw tote received → batch identity checked → product weighed → visual sorting → outer leaves removed → manual trimming → cutting → first wash → controlled wash or sanitation stage → rinse where applicable → inspection → dewatering → weighed into containers → transferred to the next controlled area.
Each arrow represents a transfer that may consume labor, create waiting time or expose product to a different hygiene condition. Each task should have a defined input, output and acceptance criterion.
Film or time several cycles if site policy allows. Start and stop points must remain consistent. “Cutting time” might mean blade-running time, operator-attended time or total elapsed time from first container arrival to final cleanup. These values answer different questions and should not be combined.
Separate touch time from elapsed time
Touch time is the time during which an operator or machine actively works on the product. Elapsed time includes processing, waiting, movement, inspection holds and interruptions. A batch may require only 18 minutes of active washing but remain in the preparation area for 55 minutes because it waits before and after the washer.
Both values matter. Touch time supports labor and equipment calculations. Elapsed time reveals WIP exposure, scheduling instability and the risk of missing downstream production windows. Reducing a three-minute cutting operation will have little commercial value if the cut product waits for 40 minutes before washing.
Classify Data Quality Before Trusting the Numbers
Many equipment projects begin with statements such as “we process about five tons per day” or “six people normally work here.” These may be useful starting points, but they are not equivalent to batch weights, payroll records or timed observations.
Assign a data-quality class to every important project input:
| Data Class | Definition | Examples | How It Should Be Used |
|---|---|---|---|
| A — Directly measured | Captured through a defined method during the audit | Calibrated batch weight, timed cycle, measured water flow, recorded acceptable output | Suitable for baseline calculations when the sample is representative |
| B — Verified record | Taken from controlled plant records and reconciled with production | Shift sheets, labor attendance, material issue records, quality results, sanitation logs | Useful for historical comparison and variation analysis |
| C — Informed estimate | Provided by experienced personnel but not yet independently verified | Typical cleaning time, peak product mix, expected new-customer volume | May support preliminary planning but requires sensitivity analysis |
| D — Unresolved assumption | Provisional value without adequate evidence | Future SKU mix, assumed yield, supplier capacity claim, unconfirmed utility availability | Must be highlighted as an open item before final equipment selection |
A common mistake is to average high-quality and low-quality inputs into one precise-looking model. A measured cycle time multiplied by an unverified annual volume does not create an audited annual saving. Keep assumptions visible and test how the conclusion changes when they change.
Build the Observation Sheet Around Material, Time and Quality
Each observed batch should have a unique record. At minimum, capture the following fields:
| Audit Area | Fields to Record | Why the Fields Matter |
|---|---|---|
| Product identity | SKU, ingredient, supplier or source, variety, batch, receipt date, temperature and raw condition | Explains variation that cannot be attributed to operators or equipment |
| Finished specification | Cut size, trim standard, defect tolerance, moisture target, pack or transfer format and intended use | Prevents comparisons between outputs that do not meet the same requirement |
| Mass balance | Raw input, acceptable output, necessary trim, avoidable loss, rejects, rework and recoverable by-product | Shows where raw-material value is retained or lost |
| Time | Setup, processing, waiting, transfer, inspection, changeover, cleaning and unplanned stoppage | Separates productive work from delay and support work |
| Labor | People by task, active minutes, supervisory support, sanitation labor and maintenance intervention | Supports labor-hour and cost calculations without assuming all assigned workers are continuously productive |
| Quality | Cut conformance, bruising, breakage, peel remaining, foreign material, excess moisture and downstream complaints | Ensures that higher speed is not mistaken for better performance |
| Flow and space | Queue size, container count, travel distance, crossings, floor area occupied and holding conditions | Reveals WIP accumulation, excessive handling and layout constraints |
| Controls | Batch identification, process checks, wash-water monitoring, corrective actions and record completion | Shows whether the operation is controlled and traceable |
Use common units throughout the audit. Record kilograms rather than alternating between kilograms, crates and portions unless a verified conversion is available. If production plans in meals or packs, retain those commercial units but connect them to a measured ingredient mass per unit.
Calculate the Baseline With Repeatable Metrics
The audit does not require complicated software. A disciplined worksheet using consistent definitions is usually more useful than a sophisticated model built on weak inputs.
Usable yield
Usable yield (%) = Acceptable output mass ÷ Raw input mass × 100
Acceptable output must meet the finished specification. Product that requires additional trimming or sorting should not be counted as acceptable merely because it remains physically present.
Sustainable throughput
Sustainable throughput (kg/h) = Acceptable output mass ÷ Total operating hours
Total operating hours should reflect the defined scope. If the objective is shift planning, include routine minor stops and product-related delays but report breaks, major failures and cleaning separately. If the objective is machine performance, also calculate running throughput using only active processing time. Label the two figures clearly.
Labor hours per 1,000 kilograms
Labor hours per 1,000 kg = Total direct preparation labor hours ÷ Acceptable output kg × 1,000
Include operators who load, unload, transfer, inspect and support the process. A cutter attended by one person may still depend on two additional workers staging and removing containers.
Preparation cost per kilogram
Preparation cost/kg = Direct labor + consumables + water and energy + waste handling + allocated maintenance + relevant overhead ÷ Acceptable output
Keep cost categories visible rather than reducing everything immediately to one total. The proposed solution may reduce direct labor while increasing maintenance, sanitation chemicals, spare-parts inventory or energy use.
Downtime rate
Downtime rate (%) = Unplanned stopped time ÷ Planned available production time × 100
Record the reason for each stop. Material shortage, blocked discharge, cleaning, blade adjustment, safety intervention and mechanical failure require different corrective actions.
On-time preparation rate
On-time preparation rate (%) = Batches available by required handover time ÷ Total scheduled batches × 100
This metric connects the preparation area to the actual customer of the process: cooking, mixing, assembly or packaging. High kilograms per hour do not compensate for ingredients arriving after the downstream batch has started.
Illustrative Calculation: What the Baseline Can Reveal
Consider a hypothetical central kitchen preparing cut vegetables for ready-meal production. During an observed shift, 2,400 kilograms of raw vegetables enter the preparation area. The operation produces 1,944 kilograms of acceptable output, uses 54 direct labor hours and runs for seven scheduled production hours excluding the final sanitation period.
- Usable yield = 1,944 ÷ 2,400 × 100 = 81%
- Sustainable output = 1,944 ÷ 7 = approximately 278 kg/h
- Labor hours per 1,000 kg = 54 ÷ 1,944 × 1,000 = approximately 27.8 hours
The process map shows that the cutting station can produce 480 kilograms per running hour, but washing and inspection together sustain only 300 kilograms per hour for this product mix. Workers respond by building a queue of cut product. The preparation area therefore does not have a 480 kg/h sustainable line merely because its cutter reaches that rate.
Suppose 160 kilograms of the 456-kilogram mass difference is necessary skin, root, core and defect removal under the agreed specification. The remaining difference cannot automatically be called avoidable waste. It may include soil removed during washing, water drainage, rejected raw material, sampling variance and weighing error. A second mass-balance study is needed before a yield-improvement claim can be made.
This example is an audit model, not a performance benchmark or promised result. It demonstrates why acceptable output, line balance and loss categories must be measured together.
Audit Raw-Material Variation, Not Only Average Volume
Agricultural raw materials are variable production inputs. Lettuce harvested in wet conditions may carry more soil and free water. Stored potatoes may have different firmness, sprouting or defect levels. Carrot diameter influences orientation and cutting output. Leaf strength affects breakage during agitation and transfer.
Create a raw-material condition code that operators can apply consistently. The code might classify size distribution, soil load, maturity, firmness, temperature, visible defects and packaging condition. Compare throughput, yield and rework across the condition classes.
This distinction protects both the facility and the equipment supplier. Without it, a difficult incoming batch may be interpreted as machine underperformance, while a carefully selected trial batch may create an unrealistic expectation for normal production.
Seasonality should also appear in the equipment brief. If the line must handle a wide size range, the solution may need adjustable settings, alternative tooling, pre-grading or a parallel manual exception route. Designing only for the easiest raw material can create frequent stoppages and product damage during the rest of the year.
Measure Quality at the Point Where It Is Created
Quality inspection at the end of the line identifies defects too late to explain them. Audit quality after every operation capable of changing the product.
After trimming or peeling, separate necessary removal from sound edible material removed through over-trimming. After cutting, measure the proportion meeting the agreed dimension and record fines, broken leaves, crushed edges and pieces requiring recutting. After washing, inspect for remaining soil, foreign material and physical damage. After dewatering, assess surface moisture, clumping, bruising and product temperature where relevant.
Cut consistency has downstream consequences. Uneven pieces may cook at different rates, absorb seasoning differently or create inaccurate portions. Excessive dewatering force can damage delicate leaves, while inadequate moisture removal may affect weighing, dressing adhesion, packaging performance and product quality. The audit should connect each specification to its downstream reason rather than treating visual uniformity as an isolated target.
Separate RTC and RTE Requirements During the Audit
Ready-to-cook and ready-to-eat products should not be treated as interchangeable simply because they use similar vegetables or equipment. An RTC ingredient is intended to receive a later cooking step, although the actual process and hazard controls must still be defined. An RTE fresh-cut product may be consumed without a later microbial kill step.
For RTE products, the audit should pay closer attention to hygienic zoning, personnel and utensil movement, post-wash exposure, wash-water controls, equipment cleanability, environmental conditions, cold handling and protection from raw-product traffic. Washing and antimicrobial treatment may reduce contamination under controlled conditions, but they do not sterilize produce or replace preventive food-safety controls.
Record every point where raw incoming material, waste containers, employees, tools, water, mobile equipment or drainage could cross into a cleaner post-wash area. A faster line that preserves an unsuitable crossing is not a complete solution.
If RTC and RTE products share rooms or equipment, document the production sequence, separation method, sanitation procedure, verification activities, time required and authority for release. The equipment brief must reflect these operating controls. It should not assume that stainless-steel construction alone makes shared production appropriate.
Include Sanitation and Changeover in Capacity
Sanitation time is operating time required to produce food safely; it is not an external inconvenience that can be removed from every capacity calculation. Record dry removal, pre-rinse where applicable, disassembly, cleaning, rinsing, sanitizing, inspection, reassembly, verification and release as separate activities.
Observe which surfaces are difficult to reach, where food accumulates, whether covers and belts can be opened safely, how parts are handled during cleaning and whether cleaning creates splash or aerosol exposure near already-clean areas. Also record the tools, water pressure, chemical control, drainage and number of employees required.
A machine that processes product rapidly but takes several hours to disassemble may be unsuitable for a multi-SKU central kitchen. Conversely, a highly flexible machine may still require long changeovers when blades, belts, water circuits or allergen controls must be changed and verified.
Changeover should be divided into product removal, tooling change, setting adjustment, cleaning, inspection, test output and release. This reveals whether the delay comes from the equipment, the sanitation program, missing tools, poor scheduling or approval procedures.
Audit Ergonomics and Occupational Safety Alongside Output
Manual preparation can involve repetitive knife work, prolonged standing, lifting wet containers, awkward reaching and frequent movement across slippery floors. Equipment can reduce some exposures while introducing rotating blades, pinch points, electrical systems, chemical handling and unexpected startup risks.
Record container weights, lift heights, reach distances, repetitive motions, knife use, floor conditions, traffic conflicts and the frequency with which workers clear jams or retrieve product. Pay particular attention to behaviors that indicate the current method is difficult to operate, such as removing guards, reaching into equipment, carrying overloaded totes or cleaning before energy has been isolated.
The future equipment brief should define guarding, safe feeding, emergency-stop access, cleaning isolation, operator platforms, container presentation and maintenance access. Training and supervision remain necessary after installation. Automation changes the skill profile; it does not remove human responsibility.
Find the Real Line Constraint Through WIP and Line Balance
Work-in-process is material that has entered preparation but has not reached the defined finished handover point. Count containers and weigh representative queues at regular intervals. Record the time and location of the highest accumulation.
A queue before a station usually indicates that the station or its operating rule cannot absorb upstream flow. A queue after a fast machine may indicate inadequate downstream capacity. No visible queue can also be misleading when upstream workers are deliberately slowed to prevent accumulation.
For each stage, calculate:
Required stage input = Required acceptable downstream output ÷ Stage yield
If a line must deliver 600 kilograms per hour of acceptable cut product after a stage with a verified 90% yield, that stage requires approximately 667 kilograms per hour of input. Upstream processes must supply that input under the same operating schedule.
Compare sustainable stage capacity rather than catalog ratings. The lowest sustainable capacity normally constrains the line, but batch timing, parallel machines, buffer limits and changeover sequences may create additional constraints. A balanced design does not require identical equipment ratings. It requires each stage to support the production plan without uncontrolled queues, starvation or product-quality deterioration.
Compare Manual, Semi-Automatic and Integrated Options
| Decision Factor | Manual Process | Semi-Automatic Configuration | Integrated Processing Line |
|---|---|---|---|
| Product volume | Suitable for low or intermittent volumes | Useful where selected repetitive tasks have stable demand | More defensible when sustained volume can utilize connected equipment |
| SKU complexity | Flexible for irregular products and frequent small batches | Allows mechanized core tasks with manual exception handling | Requires planned recipes, settings, routes and changeovers |
| Labor profile | Depends heavily on trained operators and attendance | Can reduce repetitive work without eliminating inspection and handling | Shifts labor toward feeding, monitoring, quality, sanitation and maintenance |
| Space and utilities | Lower fixed utility demand but may occupy substantial table and WIP space | Can fit existing rooms if access and service points are adequate | Needs coordinated layout, drainage, power, water, waste and access planning |
| Quality control | Relies strongly on individual technique | Can standardize selected dimensions or process conditions | Supports repeatable settings but still requires raw-material control and verification |
| Changeover | Usually fast for small tools, although labor-intensive cleaning may remain | Depends on tooling and cleaning requirements | Can become a major capacity loss when product mix changes frequently |
| Operational risk | Absence and skill variation can disrupt output | Creates dependence on selected machines and trained operators | Creates connected-system, maintenance and line-stop risks |
Manual processing remains reasonable when demand is low, batches are small, products vary widely or visual judgment dominates the task. Semi-automation is often appropriate when one stable, repetitive operation—such as cutting, peeling, washing or dewatering—can be improved without redesigning the entire room.
An integrated line becomes more credible when demand is sufficiently stable, multiple stages must be balanced, manual transfers create unacceptable delays, hygiene separation requires controlled flow and the facility can support the required utilities, sanitation and maintenance. The decision should follow the audited production requirement, not a preference for the highest automation level.
Translate Audit Findings Into an Equipment Brief
The most useful result of the audit is a requirements document that suppliers can interpret and test. It should define outcomes and constraints before naming specific machine models.
Raw-material definition
- Ingredient and variety
- Size and weight distribution
- Incoming temperature and packaging
- Soil, defect and maturity condition
- Seasonal or supplier variation
Finished-product definition
- Cut, peel, trim or portion specification
- Acceptable and unacceptable defects
- Required moisture condition
- Intended RTE, RTC, cooking or packaging route
- Transfer container, batch size and downstream demand pattern
Capacity requirement
- Required acceptable output by SKU or product family
- Peak hourly and shift demand
- Available production window
- Target utilization and growth scenario
- Maximum acceptable queue or holding time
Operating conditions
- Available floor space and ceiling height
- Door, corridor and installation access
- Electrical supply, water, drainage, compressed air and ventilation
- Room temperature and wet-area conditions
- Cleaning method, sanitation window and verification requirements
Commercial and service requirements
- Expected operating days and annual volume
- Labor and material cost assumptions
- Maintenance skills available on site
- Critical spare-parts expectations
- Product testing and acceptance criteria
- Required documentation, training and after-sales support
Separate mandatory requirements from preferences. “Output must meet a 10 mm dice specification” is different from “the machine should have a touchscreen.” This distinction allows suppliers to propose technically different solutions without losing the core operating objective.
Evaluate the New Risks Created by Automation
Automation can concentrate production through fewer assets. If a critical cutter or washer stops, the effect may spread across several downstream products. Audit the current fallback routes and decide whether the future operation needs spare capacity, parallel modules, manual contingency procedures or critical spare parts.
Connected equipment may also create hidden sanitation zones, longer startup checks, more complex guarding and greater dependence on trained maintenance personnel. Increased speed can generate product damage or overwhelm inspection and packaging. Recirculated water systems require defined monitoring and control. Poorly designed transfers may drop, compress or trap the product.
These risks do not make automation unsuitable. They belong in the comparison so that the proposed system is evaluated as an operating process rather than a collection of purchase prices.
Model ROI Without Turning Assumptions Into Promises
A basic payback model can be prepared after the current baseline and proposed process are defined:
Annual net benefit = Avoided labor cost + verified material-value improvement + avoided outsourcing or overtime + incremental contribution from realizable additional output − added operating and maintenance costs
Simple payback period = Installed project investment ÷ Annual net benefit
Only include additional output when sales demand, downstream capacity and supply availability can support it. A line capable of producing more does not create customer orders. Likewise, a projected yield improvement should be supported by representative product testing against the same finished specification.
Run at least three scenarios: conservative, expected and high-demand. Vary utilization, labor redeployment, yield, maintenance, changeover time and raw-material cost. If the investment is justified only under the most optimistic scenario, the project may require a smaller scope or staged implementation.
Common Workflow Audit Errors
- Using daily totals without SKU detail: Different products create different loads, yields and changeovers.
- Timing only the fastest cycle: Demonstration speed does not represent sustainable shift output.
- Ignoring operators around the machine: Loading, inspection, transfer and sanitation remain part of the labor requirement.
- Counting all mass loss as waste: Necessary trimming, soil, water and rejects must be separated from avoidable product loss.
- Auditing production but not cleaning: Sanitation and changeover can determine usable capacity.
- Combining RTE and RTC assumptions: The absence of a later kill step changes risk and process-control requirements.
- Accepting rated capacity as line capacity: Sustainable output depends on the product, specification, feeding, downstream stages and stoppages.
- Hiding uncertainty in averages: Data quality and observed variation should remain visible.
- Selecting equipment before defining acceptance criteria: A test cannot confirm success if acceptable output has not been defined.
When Automation Should Be Delayed or Limited
Automation should be delayed when the product range, finished specifications or demand forecast remain unresolved. Equipment cannot stabilize a business model that changes every week without defined priorities. The operation may benefit more from standardized work, production scheduling, raw-material specifications, simple weighing controls or improved container flow.
Manual work may remain commercially appropriate for low-volume specialty products, irregular ingredients and tasks requiring frequent visual decisions. A parallel manual route can also handle exceptions that would otherwise force an expensive line to accommodate every possible product.
Semi-automatic equipment may be the better choice when the audit identifies one repeatable burden but the surrounding workflow remains flexible. A cutter, peeler, washer or dewatering unit can be introduced with controlled buffers and measurable acceptance criteria. The facility can validate demand, operator capability, sanitation and maintenance before connecting more stages.
Full-line automation should be considered only when the required output, product families, changeover strategy, hygiene zoning, utilities, maintenance plan and downstream capacity are sufficiently defined. Even then, equipment cannot replace process design, food-safety management, preventive maintenance, supervision or training.
From Workflow Observation to a Defensible Project Scope
The purpose of a food preparation workflow audit is not to produce more paperwork. It is to stop uncertain assumptions from becoming fixed equipment decisions.
A useful audit shows how raw material becomes acceptable output, where time and yield are lost, which observations are reliable, how RTE and RTC risks differ, what sanitation consumes and how each stage interacts with the rest of the line. It also recognizes where manual judgment remains valuable.
With that baseline, the project team can compare process changes, standalone machines, semi-automatic modules and integrated lines using the same production requirement. Suppliers receive measurable inputs instead of a broad request for “more automation.” Product tests can be designed around defined acceptance criteria. Layout discussions can account for people, waste, water, WIP, maintenance and cleaning—not merely the external dimensions of machines.
The central lesson is straightforward: food preparation automation is a process redesign decision. The equipment is one part of that redesigned process, not the starting definition of it.
Download the Workflow Audit Template
Use the Workflow Audit Template to document raw materials, product specifications, labor, yield, sustainable throughput, sanitation time, changeovers, WIP, data quality and unresolved project assumptions. The completed worksheet can support an internal investment review or become the starting input for a preliminary line concept.
When your baseline is ready, TEEMYEAH can review the process as a customized food preparation solution provider. Share representative ingredients, finished-product requirements, current and target capacity, available layout, hygiene classification and production schedule to discuss capacity matching, raw-material testing, equipment configuration and a customized layout. The resulting recommendation may involve process improvements, phased automation or an integrated food pre-processing line, depending on the evidence collected.
FAQ
1. What is a food preparation workflow audit?
A food preparation workflow audit is a structured assessment of how raw ingredients move through sorting, trimming, peeling, cutting, washing, dewatering, inspection and transfer. It records material quantities, labor, time, yield, quality, waiting, sanitation, changeovers and process-control requirements. Its purpose is to establish a reliable operating baseline before equipment is specified. Unlike a general process map, the audit distinguishes measured facts from estimates and converts the findings into capacity, hygiene, layout and performance requirements that equipment suppliers can evaluate.
2. How many production days should be included in the audit?
The audit should cover enough production periods to represent normal demand, a meaningful peak and relevant product variation. Three observation periods may provide a useful starting point, but more may be required when SKU mix, supplier condition or seasonal raw materials change substantially. The important requirement is representativeness, not a fixed number of days. If peak production cannot be observed directly, historical records and operator estimates may be used, but they should be labeled according to their data quality and tested through sensitivity scenarios.
3. What information should be measured before buying food processing equipment?
Measure raw input, acceptable output, yield categories, processing time, waiting time, labor by task, changeover, sanitation, stoppages, product damage, cut or trim conformance, queue size and downstream demand. Also document raw-material dimensions, condition, temperature, finished specifications, available utilities, floor space, access and hygiene classification. These inputs allow suppliers to evaluate sustainable capacity rather than relying on nominal kilograms per hour. Future demand and new SKUs should remain separate from the measured baseline until their assumptions are confirmed.
4. What is the difference between rated capacity and sustainable throughput?
Rated capacity is a stated output under defined or sometimes limited operating conditions. Sustainable throughput is the acceptable output that the complete process can maintain with the actual product, operators, feeding method, inspection, transfers, routine stops and downstream constraints. A cutter may run at a high instantaneous rate while the line produces much less because washing or packing cannot keep pace. Equipment comparison should therefore consider tested running capacity, sustainable stage capacity and final acceptable line output as separate values.
5. How should labor productivity be calculated in manual food preparation?
Calculate total direct labor hours used to produce an identified quantity of acceptable output. Divide the labor hours by acceptable kilograms and multiply by 1,000 to obtain labor hours per 1,000 kilograms. Include loading, unloading, inspection, internal transfer, routine setup and other work required by the process, not only the person performing the central operation. Report sanitation labor separately when useful. Comparing shifts or methods is valid only when they process comparable raw materials and deliver the same finished specification.
6. How should yield loss be audited?
Begin with a batch mass balance that separates acceptable output, necessary skin or trim, defective tissue, rejects, rework, recoverable by-products and unexplained variance. Avoid labeling the full difference between input and output as waste. Soil removed during washing, surface water, sampling errors and scale differences may affect recorded mass. Where over-trimming is suspected, create a controlled reference sample that meets the same finished specification with the minimum necessary removal. Repeated batches are needed before projecting an annual material saving.
7. Why must RTE and RTC workflows be audited separately?
Ready-to-eat products may be consumed without a later microbial kill step, whereas ready-to-cook products are intended for further cooking under a defined process. This difference affects zoning, personnel movement, post-wash handling, environmental exposure, water controls, equipment sanitation and separation from incoming raw material. Similar vegetables may pass through different control systems depending on their intended use. The audit should therefore identify the product route and risk controls instead of assuming that a shared machine or room provides equivalent protection.
8. When is semi-automation better than a complete line?
Semi-automation is often more appropriate when one repetitive task has stable demand but the surrounding product mix remains variable. A standalone cutter, peeler, washer or dewatering machine may reduce a specific workload while preserving manual inspection and exception handling. It can also allow the facility to validate sanitation, maintenance, product quality and actual utilization before expanding. A complete line becomes more credible when multiple connected stages need balancing and sufficient volume exists to use the system across the available production window.
9. What should an equipment supplier receive after the workflow audit?
The supplier should receive a structured brief covering raw materials, size ranges, incoming conditions, finished specifications, required output by product family, operating hours, yield expectations, hygiene classification, changeover limits, utilities, layout constraints and downstream interfaces. Representative photographs, videos and batch records can add context. The brief should also identify which values were measured, verified, estimated or assumed. Product-test criteria must define acceptable quality, throughput, damage, cleaning and operator requirements before the test begins.
10. Can equipment eliminate food-safety and labor risks?
No. Equipment can standardize selected operations, reduce handling and support more controllable process conditions, but it cannot replace food-safety management, hygienic zoning, sanitation verification, preventive maintenance or employee training. It may also introduce rotating components, pinch points, electrical hazards, chemical-control requirements and dependence on trained maintenance personnel. A responsible project compares the risks removed with the risks created and defines guarding, isolation, cleaning, monitoring, contingency and training measures within the overall process design.
Data and Source Note
- U.S. Food and Drug Administration, Guidance for Industry: Guide to Minimize Microbial Food Safety Hazards of Fresh-cut Fruits and Vegetables, February 2008. Scope: U.S. guidance for processors of minimally processed fresh-cut fruits and vegetables, including personnel, facility and equipment design, sanitation, processing water, production controls, records and traceback. The guidance explains that cutting can remove a product’s natural protective barrier and that many fresh-cut products receive no lethal processing step. Its historical background reported 72 U.S. outbreaks associated with fresh produce from 1996 through 2006, of which 18 implicated fresh-cut produce. These figures are historical national context, not a current incidence rate or an estimate of risk for an individual facility.
- U.S. Food and Drug Administration, Food Code 2022, January 2023 version, and Retail Food Protection: Employee Health and Personal Hygiene Handbook, 2022. Scope: model provisions and educational practices for U.S. retail and food-service establishments, including restaurants, grocery stores and institutions. The Food Code is a model used by jurisdictions and is not automatically the applicable law in every location. Facilities must verify local, national and customer requirements.
- U.S. Occupational Safety and Health Administration, Young Worker Safety in Restaurants—Food Preparation, current eTool accessed in 2026. Scope: food-preparation hazards involving slicers, dicers, choppers, mixers, knives, machine guarding, slips, strains and cleaning practices, with specific attention to young workers in U.S. restaurants. It supports the audit of training, guarding, safe feeding and energy isolation but is not a complete industrial machinery compliance standard or a substitute for jurisdiction-specific occupational-safety assessment.

